


Cum mult do tu chiar știu despre filet frezare tăietori?
Procesare stabilitate
When processing difficult to machine materials such as titanium alloys, high-temperature alloys, and high hardness materials, the tap often twists or even breaks in the part due to excessive cutting force. In the processing of long chip materials, once the chip removal is not smooth, the chips will wrap around the tap or block the hole, often causing the tap to break or break in the part. Removing a broken tap is not only time-consuming and laborious, but may also damage the parts. To solve this problem, we can use a thread milling cutter. Due to the fact that the thread milling cutter gradually cuts into the material, it generates less cutting force and rarely breaks, resulting in powder like chips. Even in the event of a broken blade, due to the much smaller diameter of the milling cutter than the threaded hole, the broken part can be easily removed from the part without damaging it.
Doi
Diversificare de materiale procesate
Excelent tăiere condiții activare filet frezare tăietori la proces a gamă largă de materiale % 2c chiar ridicat duritate oțeluri astfel ca HRC65 grad % 2c titan aliaje% 2c și nichel pe bază de aliaje poate fi ușor prelucrat. Când procesare dificil la mașină materiale% 2c fir frezare oferă a convenabil mod la proces fire: 2c altfel folosind tapping va fi dificil la mașină.
Trei
Înaltă precizie în filet prelucrare
Thread milling is mostly high-speed and efficient cutting, with powder chips and no entanglement. Therefore, both the machining accuracy and surface smoothness are far higher than other thread processing methods. Because thread milling is achieved through high-speed rotation of the cutting tool and spindle interpolation to facilitate the removal of internal thread chips. Milling threads belongs to chip cutting, with short chips. In addition, the diameter of the machining tool is smaller than that of the machining thread, which can avoid the rotation line formed by the reversal of the tap (not allowed in situations with high sealing requirements). Because the original milling cutter does not have a turning line, and the tap cannot be avoided. The phenomenon of not easily forming sticky chips. For relatively soft materials, chip sticking is prone to occur during the processing, but threads require low machine power. Because thread milling is chip breaking cutting, the tool contacts locally and is subjected to small cutting forces, while the tap tool is easy to handle when damaged.
Patru
Pe scară largă aplicabilă
The same tool can be used for right/left thread machining. As long as the pitch is the same, threads of different diameters can be fabricat using the the same tool. The same thread freza cutter can be used for blind holes and through holes. W. BSPT, PG, NPT, NPTF, and NPSF can use the same thread milling cutter for both external and internal threads.
Cinci
Cele avantaje de procesare jaluzele găuri
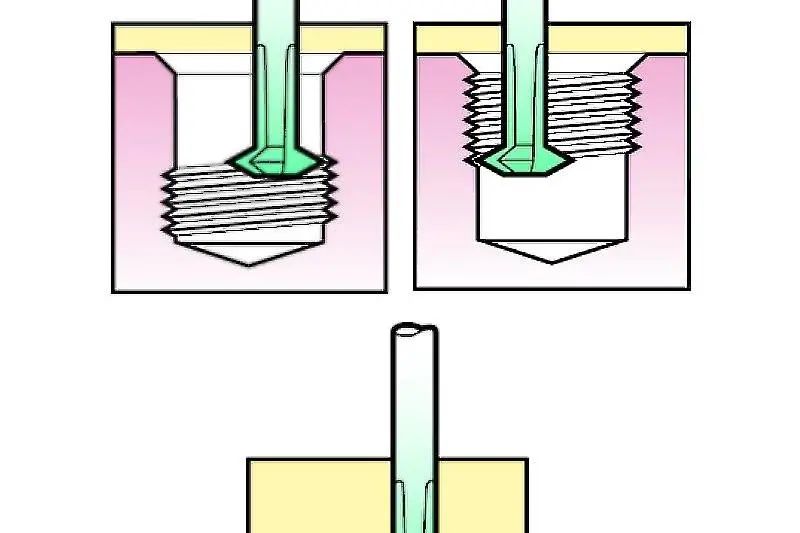
Procesare jaluzele găuri: Când freza fire, tu voi obține a complet fir contur la de fundul de gaura. Când atingerea, it este necesar la găurire mai adânc deoarece atingerea robinetului nupoate forma a complet fir contur până the third thread. Prin urmare, cu a fir frezare tăietor, tu don't nevoi la consideră schimbarea structura la adâncime gaura.
Șase
Reduce ax pierdere de mașini unelte
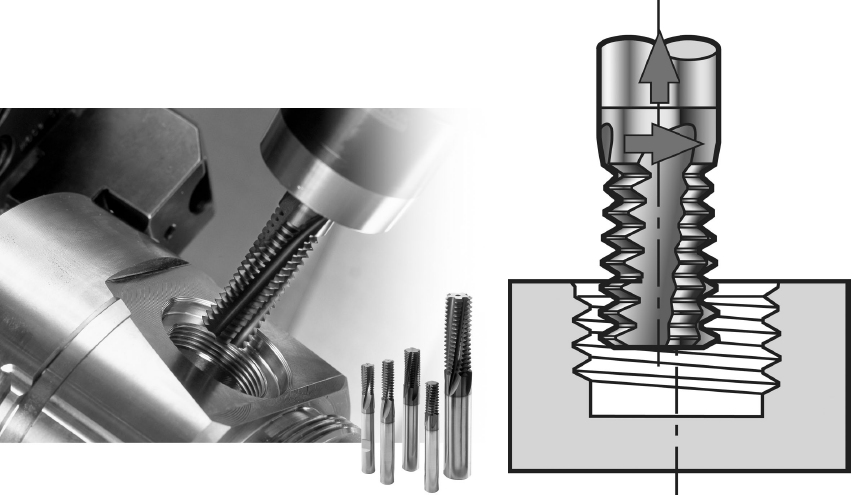
Comparat cu utilizare robinete pentru filet prelucrare, filet frezare nu necesită urgență opriri și inversări at the bottom of the the fusdle, greatly îmbunătățire the service life of the machine tool ax.
Șapte
Procesare eficiență nivel ridicat
Noi știm că în la scară largă fir prelucrare% 2c it este foarte dificil să îmbunătățiți prelucrare eficiență datorită scăzut tăiere viteză limită din robinet și înapoi instrument retractare după prelucrare filet. Cu toate acestea% 2c dacă noi folosim un fir frezare tăietor , nu numai face it au a înaltă frezare viteză% 2c dar sa mai mult canelură design crește numărul din tăiere margini , realizare it ușor de creștere alimentare rată% 2c care poate foarte îmbunătăți prelucrare eficiență. In the processing of long threads, we can also choose blades with longer blades to reduce the axial feed distance (equivalent to shortening the thread) to further improve processing efficiency;
Opt
Debavurare efect
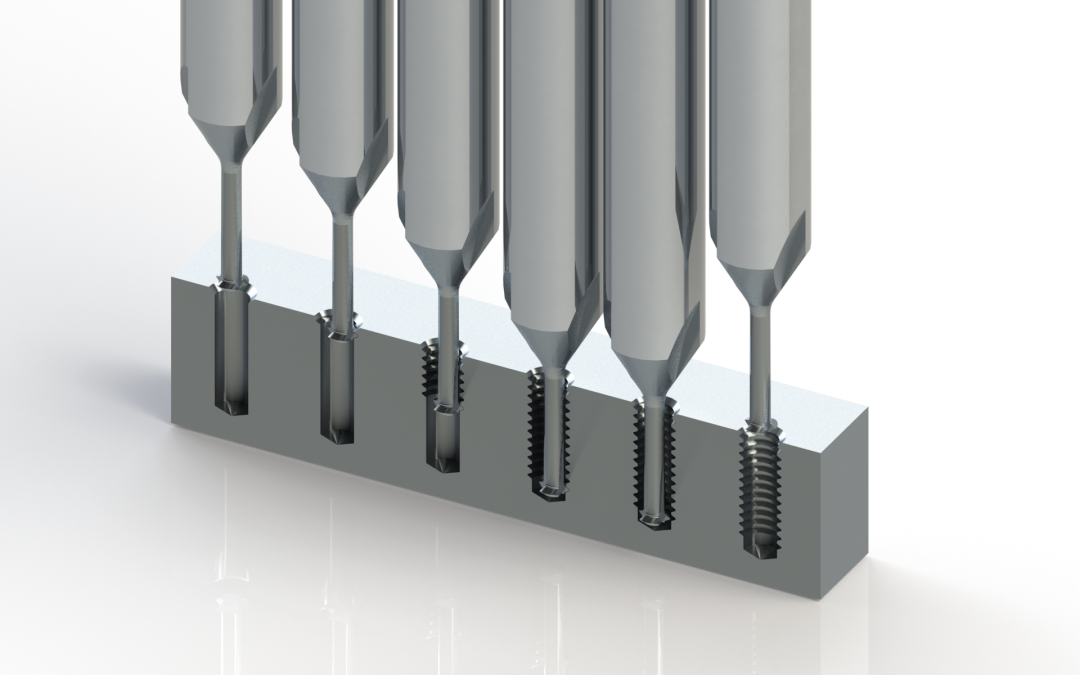
Unele mărci de fir frezare tăietori complet fir procesare și debavurare in unu du-te. Nu nevoie să cheltuiești mai multe timp pe debavurare, în timp ce economisire muncă costuri.
Nouă
Low processing cost
The thread frezare tăietor este flexibil la utilizare și poate fi potrivit pentru diverse condiții de lucru .
Pentru exemplu, we can use the same thread freza cutter to machine left-hand threads or right-hand threads; It can process both external and internal threads. All of this just requires adjusting the interpolation program. Using a tap for machining, if there are multiple threaded holes with different diameters but the same pitch on the part, different diameter taps are required. This not only requires a large number of taps, but De asemenea Takes A Longer Time To Change The Tool.
Dacă a fir frezare tăietor este utilizat% 2c as it utilizări spirală interpolare pentru prelucrare% 2c numai schimbare prelucrare program poate completa prelucrare a tuturor diametru fire, foarte economie instrument costuri și instrument schimbare timp. A asigura fir precizie robinete sunt necesare când prelucrare diferite materiale cu robinete cu robinete. Cu toate acestea% 2c acolo este nu astfel limitare când folosind a fir frezare tăietor.
The same thread freza cutter can process the vast majority of materials and achieve high-precision threads. This can also greatly reduce tool costs. When processing threads close to the bottom of blind holes, it will be difficult to obtine a complete thread at the bottom if a tap is used. Și ea este posibil că în timpul timpul timpul când jos atingeți opriți și este gata să înapoi și retrageți, the tool will continue to move forward a little distance (floating tapping), which can easy cause the tap to break.
By using a thread milling cutter, this problem can be avoided - the thread milling cutter is smaller than the hole and does not need to reverse the cutter, while still maintaining the complete thread shape at the tool tip. This way we can obtain a complete and accurate thread depth! In some machining processes, thread milling can help us solve many problems.
Pentru exemplu, in the thread prelucrare of large, non circular parts, complex clamping and balancing are required to evit vibration when machining on a strung. At this point, prelucrare can be carried out on the machining center, with the parts stationary and the thread freza cutter rotativ to evit balance issues. For example, when processing intermitent threads, vibration and impact have a significant impact on the blade and sunt predispuse la crăpături. Utilizare Utilizare A filet frezare tăietori evită mari impacturi și extinde unealta viață ca instrumentul treptat taie în material discontinuități.


